What is predictive maintenance?expand_more
Predictive maintenance is a strategy that measures the actual condition of equipment to anticipate failure before it happens and plans maintenance around that prediction. It differs from calendar-based preventive maintenance in that the timing of intervention is set by measured data rather than a fixed interval. Vibration analysis, shock pulse measurement, thermography, oil analysis and ultrasound are the most common techniques. A well-built programme markedly reduces unplanned downtime and lets spare parts and labour be planned in advance.
What is the difference between condition monitoring and predictive maintenance?expand_more
Condition monitoring is the activity of measuring and tracking equipment health: data is collected, evaluated and trended. Predictive maintenance is the management strategy that turns that data into a maintenance decision. In other words, condition monitoring is the method and predictive maintenance is the purpose it serves. A plant that performs condition monitoring but never connects the data to its maintenance plan is not practising predictive maintenance.
Which faults can vibration analysis detect?expand_more
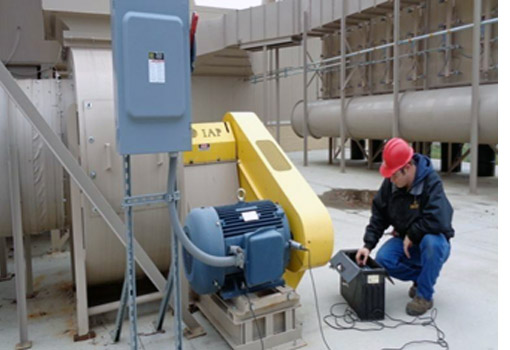
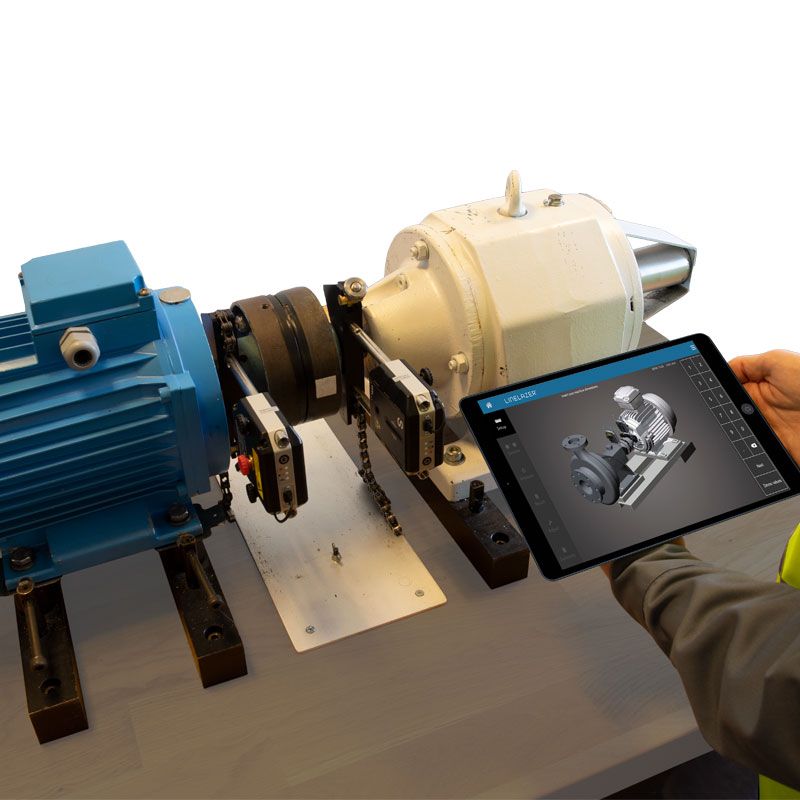
Vibration analysis detects the following faults on rotating equipment: bearing damage (inner race, outer race, ball, cage), gearbox faults (tooth breakage, wear, eccentricity), unbalance, mechanical looseness, parallel and angular misalignment, resonance, belt and pulley problems, electric motor faults (broken rotor bars, air gap eccentricity), and cavitation in pumps and fans. Each fault type has its own frequency signature in the spectrum, and diagnosis rests on recognising that signature.
What is SPM HD and how does it differ from conventional vibration measurement?expand_more
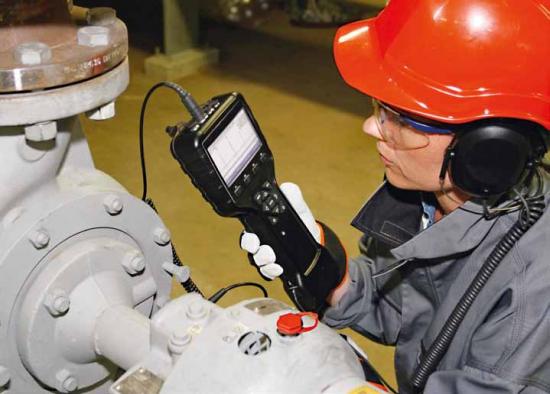
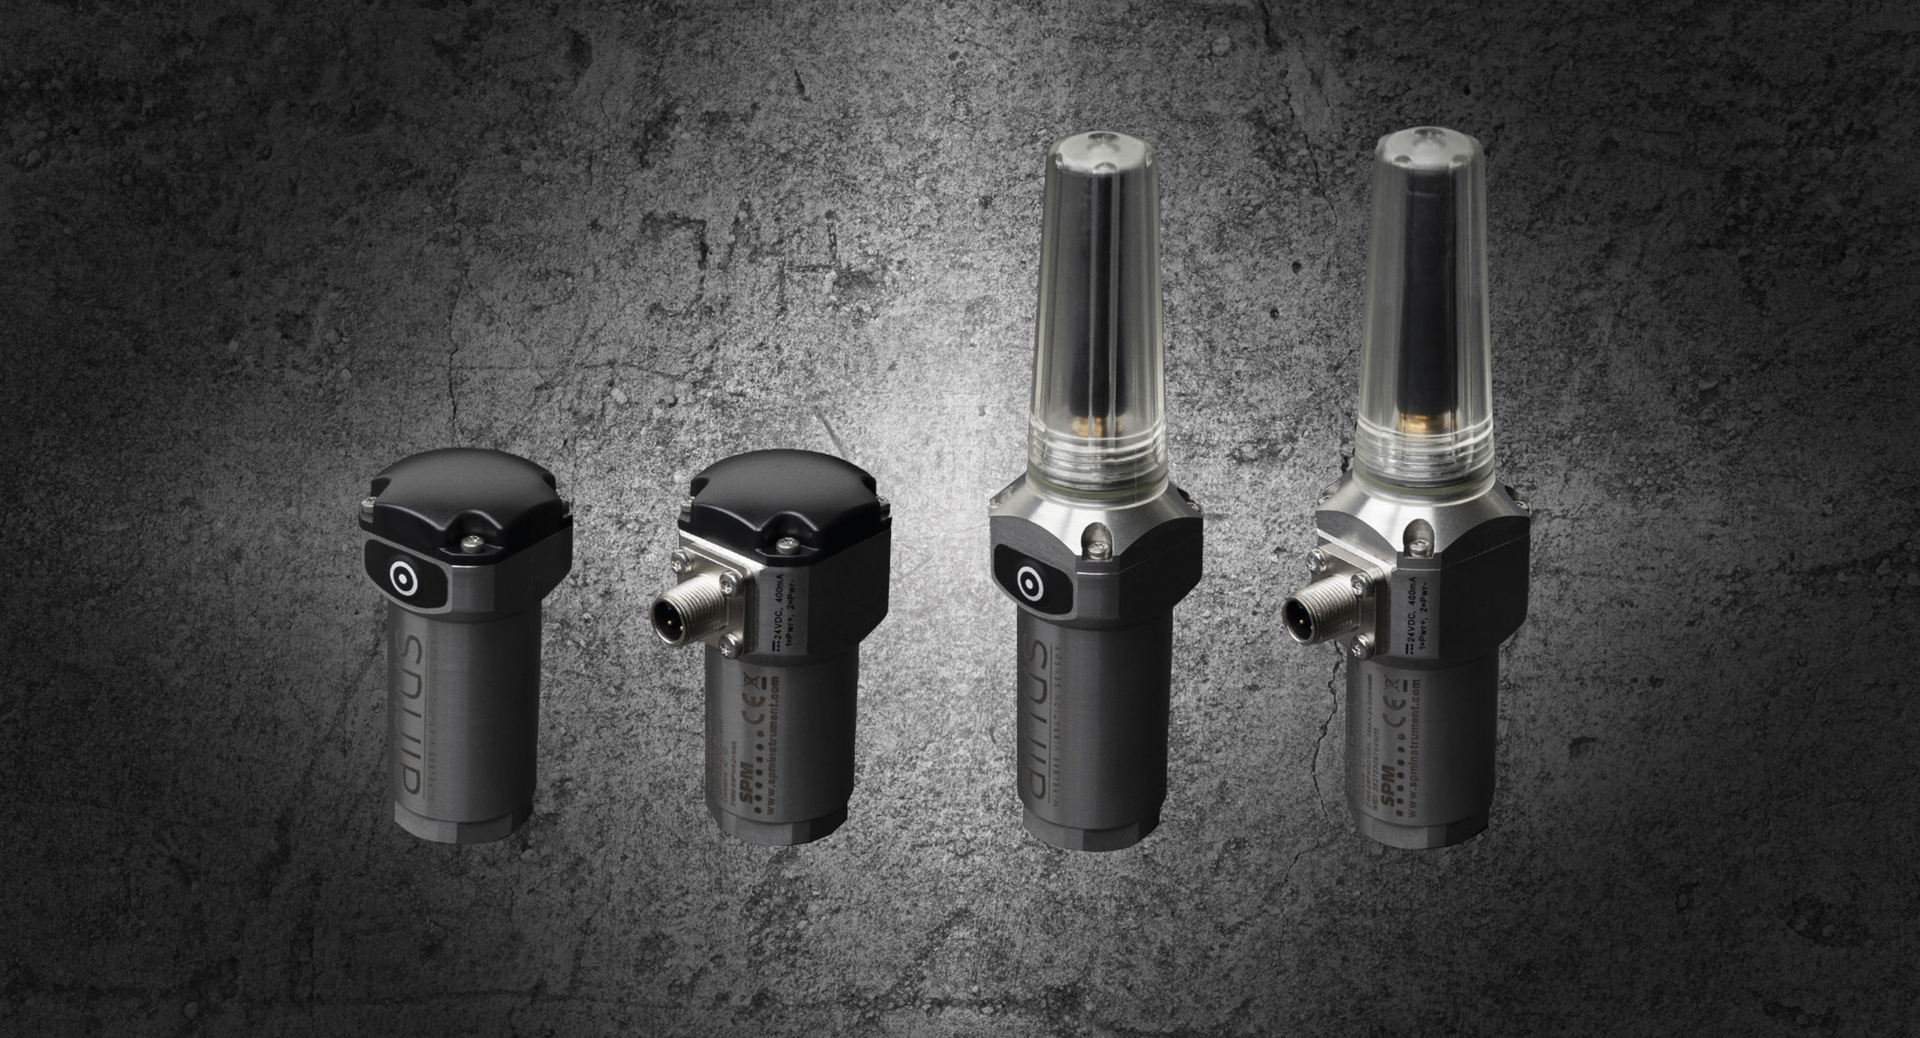
SPM HD is SPM Instrument's patented shock pulse measurement method. It measures the high-frequency shock waves produced by metal-to-metal contact on bearing surfaces, amplifying them through order-synchronous sampling and digital signal processing. Conventional vibration measurement sees the motion of the machine as a whole and becomes weak at low speed; SPM HD can detect bearing damage even at speeds as low as 0.1 rpm. The result is expressed as two decibel values: HDm (damage severity) and HDc (lubrication condition).
What are the ISO 10816 and ISO 20816 vibration limits?expand_more
ISO 10816 (and ISO 20816, which supersedes it) assesses machine vibration severity through broadband RMS velocity (mm/s), grouping machines into classes by power and mounting type. For rigidly mounted machines between 15 and 300 kW, for example, Zone A (newly commissioned) is 0–2.8 mm/s, Zone B (acceptable for unrestricted long-term operation) 2.8–4.5 mm/s, Zone C (restricted operation) 4.5–7.1 mm/s and Zone D (risk of damage) above 7.1 mm/s. Limits vary by machine class, so the relevant part of the standard and the manufacturer's instructions govern.
What is on-site balancing and when is it used?expand_more
On-site balancing is the balancing of a rotating part without removing it, in its own bearings and at operating speed. It is applied to fans, propellers, impellers, crusher rotors and rolls. Unlike workshop balancing, the rotor is balanced with its own bearings, coupling and real operating conditions, so it genuinely reduces the vibration you have on site. A dominant amplitude at 1X running speed with a stable phase points to unbalance. A typical single plane fan balance takes 2–4 hours where access is straightforward.